
*The article is sourced from the Hinalea website
One of the fastest-growing areas in food technology today is the integration of Artificial Intelligence (AI) with Hyperspectral Imaging for real-time food quality inspection. These advanced technologies enable comprehensive analysis of raw materials and finished products directly at the point of production, eliminating the need for lengthy and complex laboratory testing.
ASIO Vision is at the forefront of Industrial Imaging and Machine Vision solutions in Israel, offering advanced technologies in Machine Vision, Thermal Imaging, Hyperspectral Imaging, and AI-powered Inspection. The company focuses on helping manufacturers transition from traditional inspection methods and manual processes to intelligent, automated, data-driven quality control performed in real time.
Why Traditional Quality Inspection Is No Longer Enough
The food industry faces increasingly stringent requirements for quality, safety, and consistency throughout the supply chain. Manufacturers must detect deviations quickly, maintain consistent product quality, and respond immediately to changes in production conditions.
Despite major advances in manufacturing automation, many quality assurance procedures still rely on conventional laboratory sampling, microbiological testing, and manual inspection. While these methods provide high accuracy, they require specialized personnel and often take hours—or even days—to produce results.
For manufacturers, this translates into delayed decision-making, costly product rejection, production interruptions, and significant operational expenses. In many cases, abnormal results are identified only after products have already been packaged, shipped, or distributed.
As a result, the transition from retrospective laboratory testing to real-time quality inspection has become one of the industry's most important technological priorities.
How AI Enhances Hyperspectral Imaging
Among the most promising technologies in this field is Hyperspectral Imaging.
Unlike conventional cameras that evaluate only color, shape, or visible defects, hyperspectral systems analyze the unique spectral signature of the material itself. Rather than simply inspecting a product's appearance, they reveal chemical and physical characteristics that are invisible to the human eye.
Through spectral analysis, manufacturers can identify:
- Contaminants
- Raw material inconsistencies
- Early signs of spoilage
- Changes in chemical composition
- Variations in freshness and product quality
Hyperspectral Imaging systems capture information across hundreds of wavelengths, generating vast amounts of both spectral and spatial data.
This is where Artificial Intelligence becomes essential.
AI algorithms process this complex data in real time, recognize intricate patterns, and convert raw measurements into actionable insights. The combination of Spectral Imaging and AI creates an entirely new layer of Industrial Intelligence, where vision systems not only capture images but also understand, analyze, and interpret product conditions in real time.
LuxiLab™ – A Laboratory at the Point of Production
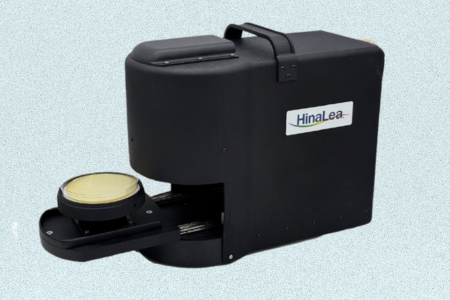
One of the newest innovations in this field is LuxiLab™, developed by Hinalea AI and recently added to ASIO Vision's portfolio of advanced inspection solutions.
Designed as a true "Lab-in-a-Box," LuxiLab™ enables real-time food quality analysis directly at manufacturing facilities, farms, logistics centers, and ports, eliminating the need to wait for external laboratory testing.
The system combines Hyperspectral Imaging, advanced spectral analysis, and AI algorithms to generate immediate insights. By collecting both spectral and spatial information from the inspected product and analyzing it using AI-based models, LuxiLab™ enables fast, accurate decision-making during the production process itself.
The platform is designed for applications including:
- Food quality inspection
- Contaminant detection
- Raw material verification
- Microbial classification
- Quality control throughout the supply chain
Its primary advantage lies in shifting quality inspection from centralized laboratories to Point-of-Need testing, delivering actionable results exactly where and when they are needed.
The Future of Food Inspection Is Already Here
The food industry is rapidly moving toward intelligent, automated, AI-driven inspection systems. The need to respond faster, reduce waste, and improve consistency across the supply chain is driving manufacturers to adopt advanced Industrial Imaging and Real-Time Inspection technologies.
The combination of Hyperspectral Imaging, Artificial Intelligence, and real-time data processing makes it possible to perform sophisticated quality analysis directly on the production line, providing immediate insights into product condition without relying on lengthy laboratory workflows.
For food manufacturers, this means improved quality control, faster response times, reduced operational risk, lower costs, and better-informed decisions throughout production and distribution.
The solutions delivered by ASIO Vision demonstrate how computer vision is evolving beyond traditional Machine Vision systems, becoming a key component of modern AI Inspection, Industrial Intelligence, and next-generation quality assurance.